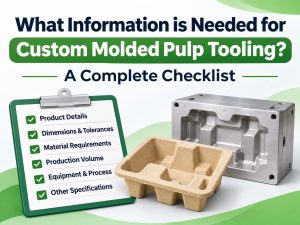
When developing pulp molded plates, tooling precision directly impacts yield rates and production stability. A high-quality mold must ensure a seamless transition across the forming, hot pressing, and trimming stages. This technical checklist outlines structural and tooling requirements to help buyers optimize plate geometry, edge design, stacking efficiency, and deformation control before initiating mold manufacturing.
1. Plate Geometry and Forming: Draft Angles and Radii
Pulp molded tableware, particularly plates, is typically manufactured using the wet pressing process, which demands a smooth finish and high structural density. During the initial product development phase, mold design must prioritize optimal draft angles and smooth surface transitions (radii) on the forming mold. Inadequate draft angles make it difficult to demold the wet-blank, significantly increasing the risk of tearing. Furthermore, poorly designed radii can lead to uneven pulp distribution. For large, thin-walled products like plates, establishing a robust structural geometry is the vital prerequisite for all subsequent manufacturing steps.
2. Troubleshooting Hot Pressing Deformation: Tooling vs. Process Variables
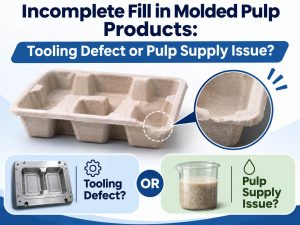
When warp or deformation occurs during a mold trial, many production supervisors immediately blame tooling accuracy. However, effective troubleshooting must isolate the variables across tooling, slurry, and equipment. Before modifying the hot-pressing mold, first verify the moisture content of the wet-blank. Uneven moisture distribution causes inconsistent shrinkage during hot pressing, leading to warping. Next, check if the hot press temperature and pressure are uniformly distributed. Only after ruling out slurry consistency and machine settings should you evaluate the mold’s exhaust hole layout and surface profile using 3D scanning.
3. Trimming Alignment: Edge Design and Mold Clearance
To achieve a clean, premium appearance, pulp molded plates require precise edge trimming. Issues like inaccurate trimming or burrs usually stem from poor dimensional alignment between the forming, hot pressing, and cutting stages. Fabricating a reliable mold requires rigorous control over the mold clearance (mold gap). With 500 pulp molding molds manufactured to date, Hanson Pulp Molding guarantees exceptional precision. We utilize high-speed CNC machining with spindle speeds up to 24,000 rpm to ensure that the cavity and trimming reference points align flawlessly, preventing edge tearing and reducing scrap rates.
4. Stacking Specifications: A Critical Metric for Logistics
A frequently overlooked requirement in the molded pulp product development checklist is stacking clearance. Plates must be densely nested during packaging, warehousing, and transportation. If the mold’s stacking angles or edge profiles are miscalculated, the plates may jam together or become damaged when pulled apart manually or by automated dispensers. Tooling engineers must calculate the exact product grammage, material thickness, and nesting angles during the prototyping stage to guarantee seamless logistics efficiency.
5. A Proven Path for Tooling and Mass Production Support
High-performance tooling requires execution that bridges design and the factory floor. Whether you are launching a new plate on Hanson equipment or integrating it into third-party production lines, we follow a strict pathway: product development → complete tooling services → mass production support. From rough machining and stress relief to finishing, 3D scanning, and assembly, we manage every manufacturing node. We don’t just ship molds; we offer on-site technical insights to help clients synchronize their forming, pressing, and trimming processes for maximum output.
-
FAQ:
-
Q1: If the molded pulp plate warps after hot pressing, is the mold defective? A: Not necessarily. While the hot-pressing mold could be misaligned, you must first verify the wet-blank moisture content uniformity, as well as the hot press temperature and pressure settings. Always rule out process variables before suspecting tooling defects.
-
Q2: How does mold design affect trimming accuracy? A: Precise trimming requires strict control over the mold clearance (mold gap) during hot pressing. Additionally, the forming stage must ensure uniform pulp thickness at the edges to prevent tearing or burrs during the mechanical cutting process.
-
Q3: Can we order new molds for non-Hanson pulp molding machines? A: Yes. We offer a “product development → complete tooling services → mass production support” pathway. Even for third-party equipment, our team optimizes the mold structure to ensure successful trials and production on your existing lines.
-
-
Ready to develop your next molded pulp plate project? Contact Hanson Pulp Molding for a comprehensive tooling evaluation and mass production support.